Our team is highly trained and experienced in servicing and producing all types of steel supplies. Need help or have a question?
sales@abrasionresistantpipe.com
Tel.: +8621-3378-0199
Our team is highly trained and experienced in servicing and producing all types of steel supplies. Need help or have a question?
sales@abrasionresistantpipe.com
Tel.: +8621-3378-0199

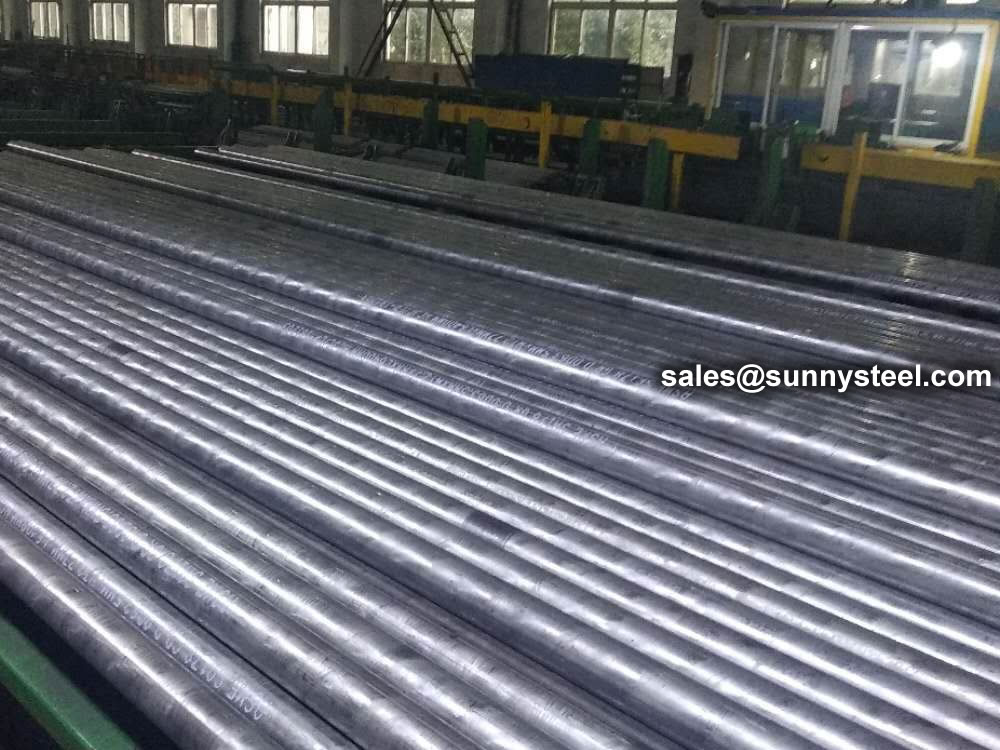
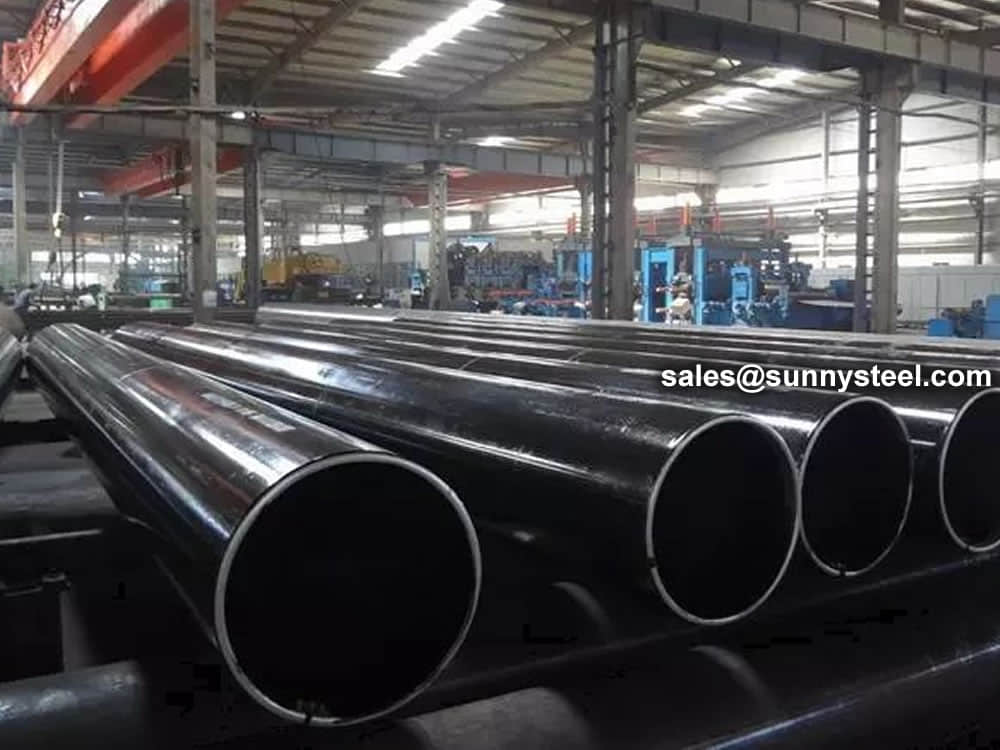
ASTM A178 tubing is carbon steel and carbon manganese ERW tubing used in boilers, boiler flues, super heaters. ASTM A178 is available in A178 Grade A (low carbon steel), A178 Grade C (medium carbon steel), and A178 Grade D (carbon manganese steel).
ASTM A178 tubing is carbon steel and carbon manganese ERW tubing used in boilers, boiler flues, super heaters. ASTM A178 is available in A178 Grade A (low carbon steel), A178 Grade C (medium carbon steel), and A178 Grade D (carbon manganese steel).
ASTM A178 standard referes to electric-resistance-welded tubes with minimum-wall-thickness. Materials are carbon steel and carbon-manganese steel, ASTM A178 pipe and tube is to be used in boiler tubes, boiler flues, superheater flues and safe ends. Steel Grades A (low-carbon steel), C (medium-carbon steel), or D (carbon-manganese steel). Manufacturing processes must include heat treatment, welding after cooling. Crush test shall be performed if required by customer.
| Grade | C | Mn | P | S | Si |
|---|---|---|---|---|---|
| Grade A Low carbon steel | 0.06-0.18 | 0.27-0.63 | 0.035 | 0.035 | ... |
| Grade C Medium Carbon Steel | 0.35 Max | 0.80 Max | 0.035 | 0.035 | ... |
| Grade D Manganess Steel | 0.27 Max | 1.00-1.50 | 0.03 | 0.015 | 0.10 Min. |
The steel shall conform to the requirements as to chemical composition prescribed in Table 1.
When a grade is ordered under this specification, sup- plying an alloy grade that specifically requires the addition of any element other than those listed in Table 1 is not permitted.
Product Analysis
1. When requested on the purchase order, a product analy- sis shall be made by the manufacturer or supplier from one tube per 100 pieces for sizes over 3 in. [76.2 mm] and one tube per 250 pieces for sizes 3 in. [76.2 mm] and under; or when tubes are identified by heat, one tube per heat shall be analyzed. The chemical composition thus determined shall conform to the requirements specified.
2. If the original test for product analysis fails, retests of two additional lengths of flat-rolled stock or tubes shall be made. Both retests, for the elements in question, shall meet the requirements of the specification; otherwise all remaining material in the heat or lot (Note 2) shall be rejected or, at the option of the producer, each length of flat-rolled stock or tube may be individually tested for acceptance. Lengths of flat- rolled stock or tubes which do not meet the requirements of the specifications shall be rejected.
| Grade | T.S. ksi [MPa] | Y.S. ksi [MPa] | EL. in 2" min. % |
|---|---|---|---|
| Grade C | 60 [415] | 37 [255] | 30 |
| Grade D | 70 [485] | 40 [275] | 30 |
Manufacture & Heat Treatment
The ASTM A178 Grade D steel shall be killed. ASTM A178 tubes shall be made by electric-resistance welding process. After welding, all tubes shall be heat treated at a temperature of 1650°F [900°C] or higher and followed by cooling in air or in the cooling chamber of a controlled-atmosphere furnace. Cold-drawn tubes shall be heat treated after the final cold-draw pass at a temperature of 1200°F [650°F] or higher.
Testing & Inspection
ERW tubes made from ASTM A178 steel may be tested or inspected in the following ways covering crush test, flattening test, flange test, tension test, reverse tension test, hydrostatic test, nondestructive electric test, dimension inspection, visual examination, as well as ultrasonic inspection.
NOTE 2—A lot consists of 250 tubes for sizes 3 in. [76.2 mm] and under and of 100 tubes for sizes over 3 in. [76.2 mm], prior to cutting to length.
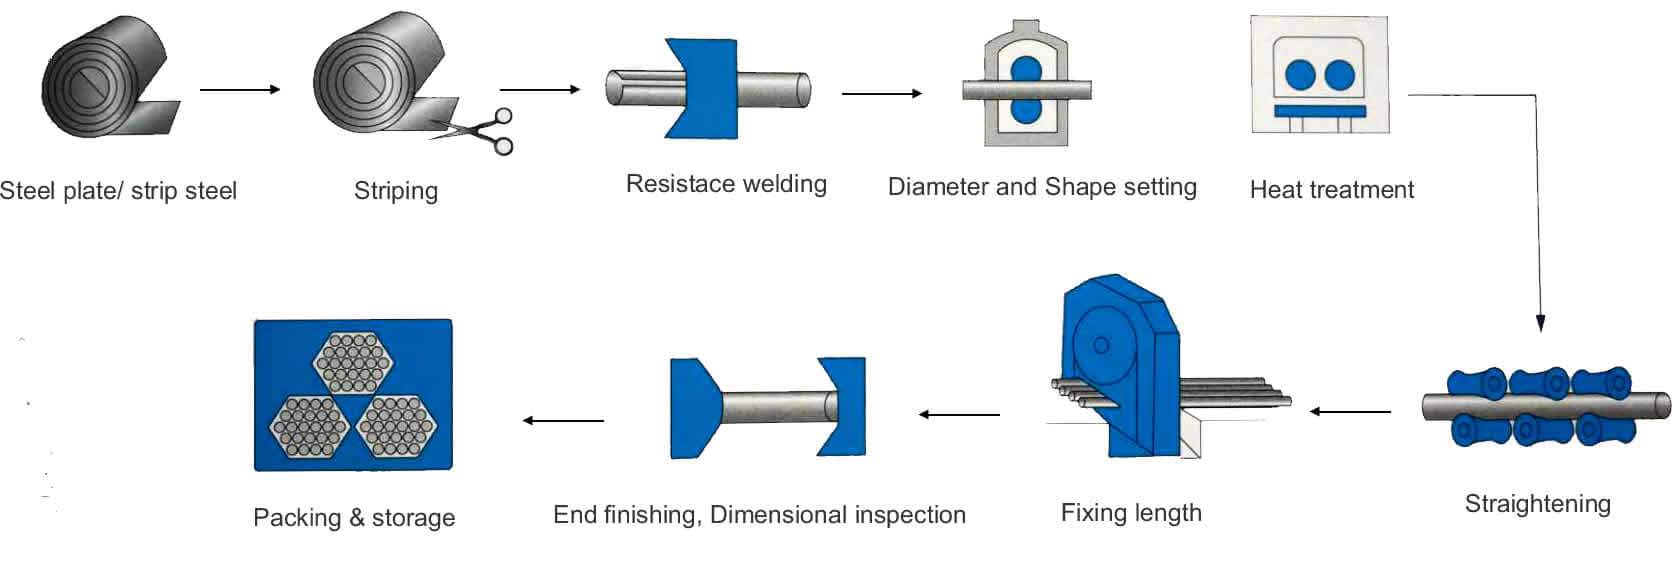
Condenser steel tube,heat-exchanger tube,low carbon steel pipe,Resistance welded steel tube ,Bolier flues,Spoerheater flues and safe ends,ERW carbon steel pipes.
Manufacturing Process: ERW
Heat treatment: After welding,all tubes shall be heat treated at a temperature of 1650°F(900℃) or higher and followed by cooling in air or in the cooling chamber of a controlled-atmosphere furnace,Cold-drawn tubes shall be heat treated after the final cold-draw pass at a temperature of 1200°F(650℃)or higher.
Surface Condition: Finished tubes shall be free of scale,A slight amount of oxidation will not be considered as scale.
Mechanical Tests Required: Flattenting Test/Flaring test/Flange test/Crush test/Tension test/Reverse Flattening test/Hydrostatic or Nondestructive Electric Test
Usage Used in boiler, superheater, heat-exchanger and pressure equipment in Petrochemical factory, Refinery factory, sugar mill, power plant, power plant, shipbuilding.